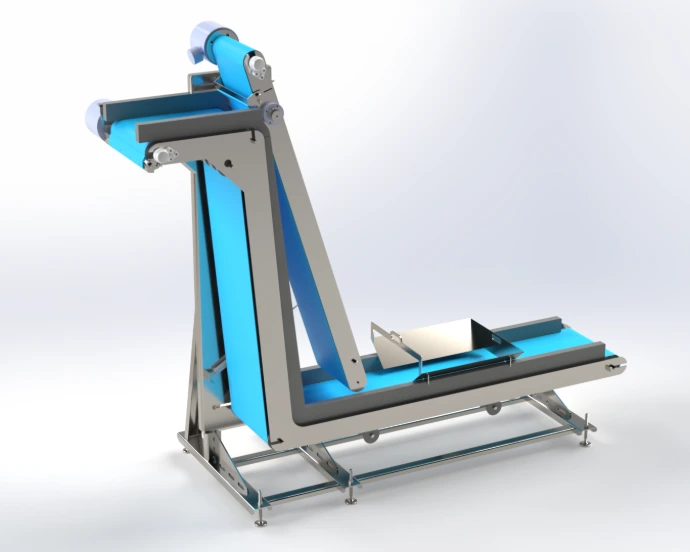
Vertical Conveyor
Vertical conveyors are designed to transport food products and materials between different elevations within a food processing or packaging facility. By moving products up or down between production levels, these systems help maximize available floor space while maintaining an efficient, continuous production flow.
Ideal for food manufacturing operations with limited space or multilevel production layouts, vertical conveyors can be integrated into processing, sorting, conveying, and packaging lines. Depending on the conveyor design, they can handle a variety of products, containers, packages, and materials while providing reliable movement between equipment and production stages.
Our vertical conveyor systems can be configured to meet specific application requirements, including product type, load capacity, conveyor speed, and facility layout. Designed for integration with existing or new production equipment, they offer a practical solution for improving material handling and streamlining manufacturing operations.
Key Benefits:
Space-Saving Design: Moves products vertically to reduce the need for long horizontal conveyor runs.
Efficient Product Transfer: Connects equipment and production areas at different elevations.
Versatile Applications: Handles a variety of food products, packages, and materials, depending on system configuration.
Customizable Configurations: Can be designed to accommodate specific production needs and facility requirements.
Production Line Integration: Connects seamlessly with other conveying, processing, and packaging equipment.
Improved Workflow: Helps
The Patriot Equipment Difference
Vertical conveyors provide food manufacturers with a reliable, space-efficient solution for moving products between production levels and optimizing overall material flow.
- Cantilever Design for fast sanitation and daily breakdown
- Forbo Endless Lug drive belting
- One-motion drive system
- Large speed range