Spiral Conveyor
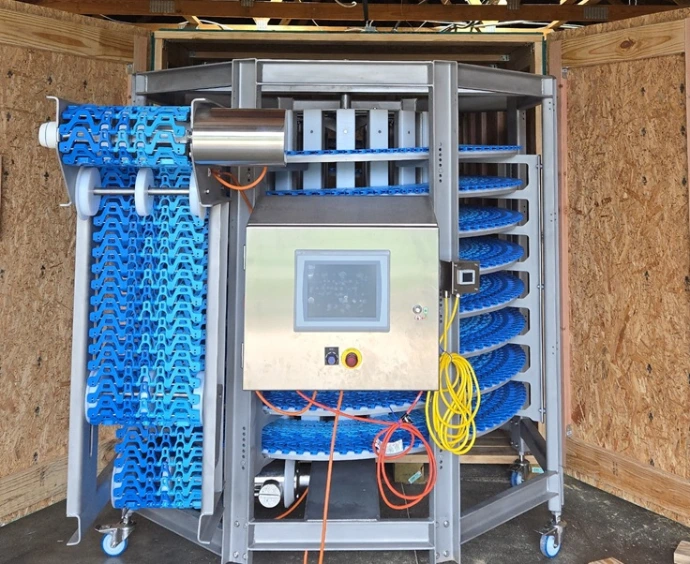
Spiral conveyors are designed to move products vertically between multiple levels of a food processing or packaging line while minimizing the floor space required. Their compact, space-saving design makes them an ideal solution for food manufacturers looking to maximize production efficiency without expanding their facility footprint.
Engineered for continuous product flow, spiral conveyors can be used for cooling, freezing, proofing, drying, or conveying products between processing and packaging operations. Their controlled movement helps maintain consistent product handling while supporting efficient production line layouts.
Designed to accommodate a wide range of food products and manufacturing requirements, spiral conveyors can be integrated into new or existing production systems. With options tailored to specific applications, they provide a versatile solution for improving material flow, optimizing available space, and supporting the demands of modern food manufacturing
Key Benefits
Space-Saving Design: Moves products vertically to maximize valuable floor space.
Continuous Product Flow: Supports efficient movement between processing and packaging stages.
Versatile Applications: Suitable for a variety of food manufacturing and handling processes.
Production Line Integration: Designed to connect with upstream and downstream equipment.
Customizable Solutions: Can be configured to meet specific product, capacity, and facility requirements
Enhance Your Experience
Spiral conveyors provide food manufacturers with an efficient, space-conscious solution for streamlining production and improving overall material handling.